BDS/05 — Tool room
Dies, tools and fixturesfor every line
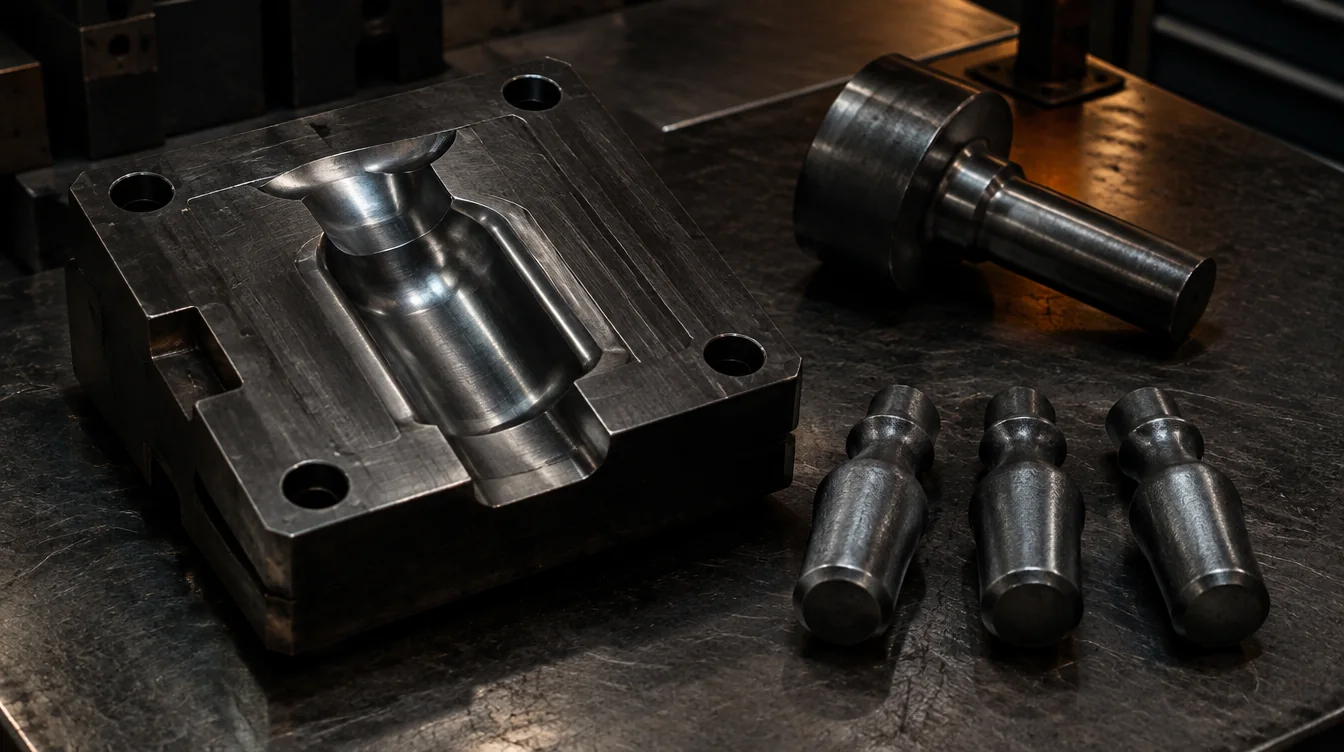
Forging quality is decided in the die. We design, cut, harden-finish and maintain our dies in-house, and use the same tool room to build the machining, inspection, assembly and test fixtures that production lines run on.
BDS/TR — What we build
Tools for our presses, fixtures for any line
The same tool room serves the forging shop and our customers: dies and trim tools for our own presses, and fixtures and gauges built to your drawing.
01
Hot forging dies
Closed-die impressions for the screw, knuckle joint and crank presses, designed against forging simulation before the die steel is cut.
02
Cold forging dies
Net and near-net shape tooling where the die, not the machine shop, holds the dimension.
03
Trimming tools
Trim and pierce tools that take the flash off straight from the forging line.
04
Machining fixtures
Workholding for turning and VMC operations, built so the part locates the same way every cycle.
05
Inspection fixtures & gauges
CMM holding fixtures and go / no-go gauges that put a part in the same datum frame every time it is measured.
06
Assembly & test fixtures
Press-fit and assembly jigs, OTA and end-of-line test nests, in metals and engineering polymers.
BDS/TR — Equipment
What the tool room runs on
Die and fixture work draws on dedicated tool-room processes and on the main machine park across the aisle.
- Wire-cut EDM
- Die inserts, punch profiles and fixture plates with sharp internal corners
- Spark (die-sinking) EDM
- Forging impressions and deep cavities in hardened die steel
- Surface grinding
- Flat, parallel die faces and fixture plates
- CNC turning & VMC milling
- Die blocks, bolsters and fixture bodies, from the main machine park
- CMM inspection
- Die and fixture verification against the CAD model
- QForm & CAD / CAM
- Forging simulation, die design and toolpath programming
BDS/TR — How a tool is made
From part drawing to approved die
01
Part & process review
Forging drawing, parting line and draft agreed; the process is simulated in QForm.
02
Die & fixture design
Impressions, trim tools and fixtures designed in CAD, with machining allowances matched to the part.
03
Die steel & machining
Die steel procured to grade, rough and finish machined on the CNC and VMC park.
04
EDM, wire-cut & grinding
Impressions sparked, profiles wire-cut and faces ground to size.
05
Trial & first-off approval
Trial forgings and first-off parts measured before the tool is released to production.
06
Maintenance log
Every die tracked for shots and refurbishment, so wear is managed before it shows on the part.
BDS/RFQ — Start a project
Need a fixture or a die?
Send the part drawing and tell us what the fixture has to hold, locate or test. We come back with a design approach and a quotation.